
Short answer: A vibratory fluid bed dryer stays reliable when you maintain five systems and trend a few simple numbers: the perforated distributor plate, the vibration drive and its springs, the dust collector and filters, the hot-air and exhaust fans with their ducts and seals, and the controls and instruments. Most problems announce themselves first as a drift in bed differential pressure, outlet moisture, vibration noise or exhaust temperature. A written checklist with daily, weekly, monthly and annual tasks, a record of baseline readings taken at commissioning, and a short critical-spares list is the cheapest way to avoid unplanned stops. The schedule below is a starting template. Always follow the manual and safety rules for your own machine.
This guide is for maintenance managers, plant engineers and owners planning the upkeep and running cost of vibratory fluidised bed dryers (VFBD) used for powders, granules, crystals and pellets. It complements our existing fluid bed dryer troubleshooting guide, which focuses on process symptoms such as channelling and poor fluidisation, and our maintenance checklists for belt dryers and rotary dryers. This guide covers the machine itself.
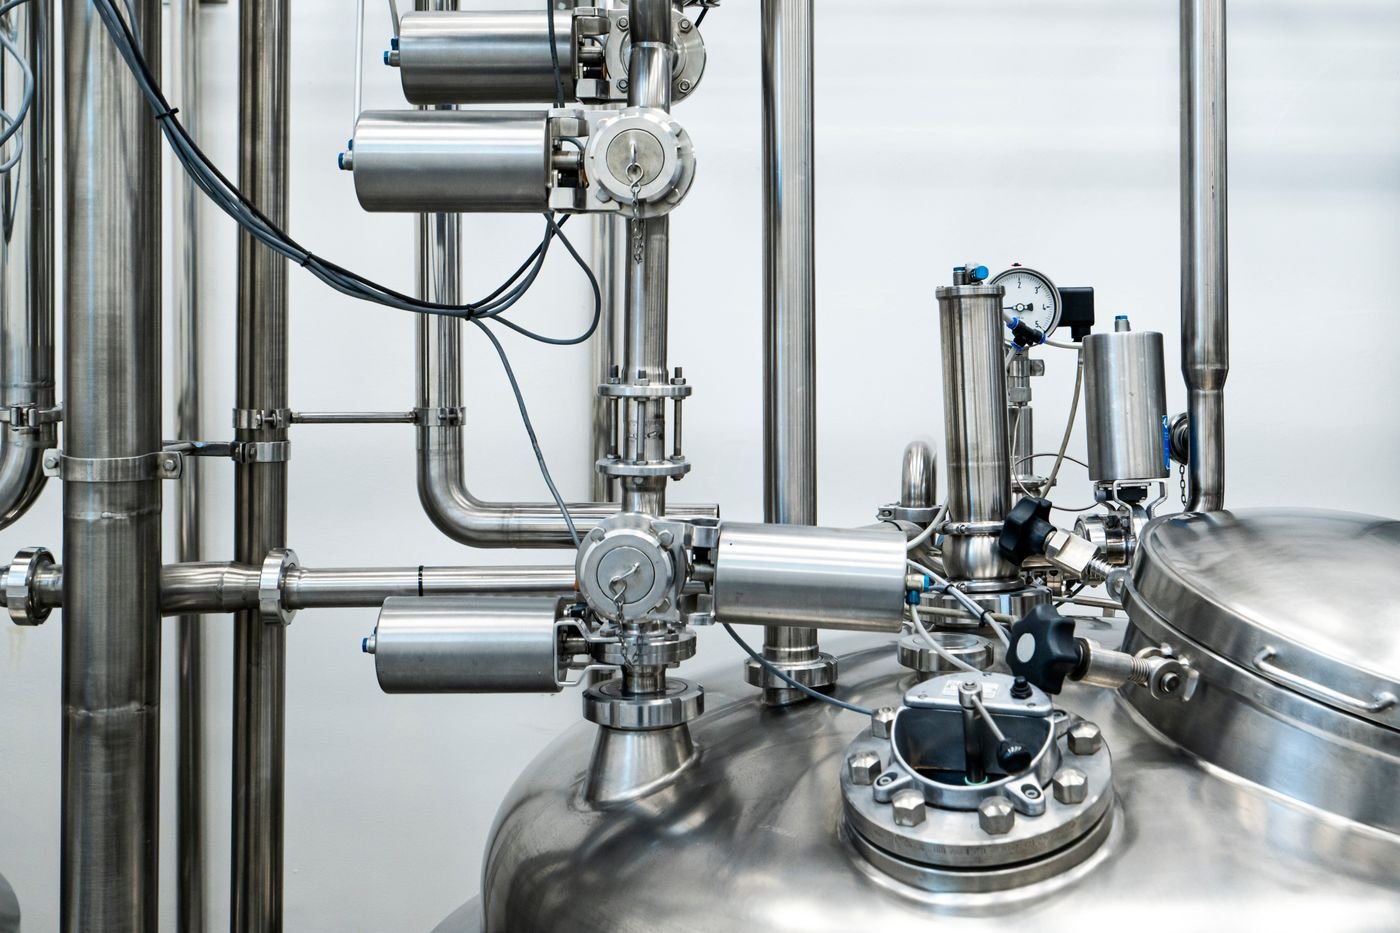
Know what you are maintaining
GTI’s vibratory fluidised bed dryer page lists the main components of a VFBD system: a vibrating fluidised bed with a perforated plate, a vibration drive system with motor and springs, hot-air generation and heating, an air distribution plenum, a product feed system, exhaust ducting and fan, a dust collection system (cyclone or bag filter) and a control panel with airflow and temperature control. Our guide to how a fluid bed dryer works explains the process, and the maintenance logic follows the component list.
Your own machine’s manual takes priority over any generic checklist. Some details, such as lubrication, bolt torque or amplitude settings, are specific to the design and must come from the manufacturer.
Safety first: isolation and dust
- Lock out and tag out before entering or cleaning any part. OSHA’s guidance on controlling hazardous energy explains the principle of isolating all energy sources before servicing (OSHA, control of hazardous energy).
- Treat dust as combustible. OSHA notes that food dusts including flour, starch, sugar, spice and feed, as well as plastics, pharmaceuticals and many chemicals, can be explosible when suspended in air (OSHA combustible dust overview). Housekeeping, ignition-source control and explosion protection decisions belong to your hazard analysis. See our dust explosion prevention guide.
- Confined space and hot surfaces. Let hot surfaces cool and follow your site entry rules.
1. Perforated distributor plate and plenum
What goes wrong: holes blocked by product or scale, residue build-up, damaged or distorted plate sections, worn weld seams, and leaks between plate and casing. Blocked areas change the air pattern and cause dead zones, wet spots and uneven moisture.
What to do:
- Record the bed differential pressure and the airflow at commissioning, at a known load, as your baseline. A rise at the same airflow and load can indicate blockage or a loaded filter, and a fall can indicate leakage or a damaged plate.
- Inspect the plate during every planned stop for blocked holes, scale and cracks, and clean as the manual allows.
- Check the plenum below the plate for product that has fallen through, which signals plate damage or poor sealing.
- For food or pharmaceutical products, follow your cleaning and changeover procedure and validation rules.
2. Vibration drive, springs and mounts
What goes wrong: spring fatigue or cracks, loose fasteners, worn motor bearings, drift in vibration amplitude, cracked supports and noise. A change in vibration changes bed movement and residence time, and therefore final moisture.
What to do:
- Record vibration amplitude or motor current at commissioning for a known product and load, then compare during routine checks, using the method the manufacturer recommends.
- Inspect springs, mounting points, supports and welds for cracks, corrosion or deformation.
- Check bolts and guards at the intervals the manual states.
- Listen for new noises and log them. Early bearing noise is cheaper to fix on a planned stop than after a failure.
- Do not run with a broken spring or loose drive; vibration forces rise quickly.
3. Flexible connections and seals
A vibrating bed connects to fixed ducts and feed or discharge points through flexible connections, which are wear items. Check for cracks, tears, loose clamps and product leakage at every planned stop. A leaking seal wastes heated air, releases dust and can pull in cold, damp air that disturbs the drying conditions. Condensation downstream can follow; see our dryer exhaust condensation guide.
4. Dust collection: cyclone and bag filter
What goes wrong: blinded or torn bags, failed cleaning cycles, blocked hoppers and discharge valves, and condensation in the collector.
The US EPA explains that as dust builds up on a fabric filter the pressure drop across it increases, so the filter material is cleaned periodically by shaking, reverse air or pulse jet, and it describes the dust cake rather than the fabric as the main collector of fine particles (US EPA, fabric filters).
What to do:
- Trend the collector differential pressure and cleaning cycle behaviour.
- Check bags or cartridges for tears, wet cake and visible dust at the clean-air outlet.
- Check the cleaning mechanism and compressed air supply if pulse-jet cleaned.
- Empty hoppers and check rotary valves and discharge points for blockage and leaks.
- Keep exhaust temperature above the dew point to prevent wet cake, using the approach in our dew point guide.
5. Fans, heater and air system
What goes wrong: fan imbalance, bearing wear, belt slip, damper drift, fouled heat exchangers or coils, failed steam traps, burner problems and air leaks. For steam and thermic fluid systems, check traps, valves and insulation; for direct-fired or electric heaters follow the supplier’s checks. The heat source selection guide explains how the choice of heating medium affects maintenance.
What to do:
- Trend inlet and outlet air temperature, airflow and fan current.
- Check dampers move freely and hold position.
- Clean or inspect coils and heat exchangers as the supplier advises.
- Look for hot spots on insulation and air leaks around doors and joints.
6. Controls and instruments
Temperature sensors, airflow measurements, pressure transmitters and the PLC/HMI all need periodic verification, because a drifting sensor can produce a stable-looking display and an off-spec product. Calibrate instruments to your quality system’s schedule, and check alarms and interlocks, including fan, heater and vibration trips, during planned stops.
A starting maintenance schedule
This table is a template, not a manufacturer’s schedule. Replace intervals with the manual’s requirements and your own failure history.
| Frequency | Tasks |
|---|---|
| Every shift or daily | Walk-round for noise, leaks and dust; check bed differential pressure, collector pressure drop, temperatures and product moisture against baseline; empty and check dust hoppers |
| Weekly | Inspect flexible connections and door seals; check dampers and visible springs and mounts; check fan belts or couplings; review alarm log |
| Monthly | Inspect bags or cartridges and cleaning system; check bolts and guards; inspect insulation and steam traps or heater; review trends |
| At each planned stop | Inspect and clean the distributor plate and plenum; inspect springs, welds and supports; inspect seals, hoppers and valves |
| Annually | Detailed mechanical inspection of drive, bearings and fans; instrument calibration; review spares and failure records; review safety systems and dust-control arrangements |
Spare parts and cost planning
Critical spares usually include vibration springs, flexible connections and gaskets, filter bags or cartridges, fan belts and bearings, a spare vibration motor or bearing set, temperature and pressure sensors, and steam trap or burner parts as relevant. Choose them from your own history and from the manufacturer’s recommendations.
Annual maintenance cost depends on product abrasiveness and stickiness, operating hours, cleaning frequency, dust loading, heating system type and how well the baseline data are used. Keep your own records of downtime and spare consumption, because they are the only reliable basis for a budget. Specific energy consumption trends, explained in our dryer energy audit guide, often reveal blocked plates, leaks and fouled coils before they cause a stop.
Questions to ask when buying a new VFBD
- What baseline data (pressure drop, amplitude, airflow) does the supplier provide at commissioning?
- Can the distributor plate and plenum be reached and cleaned without major dismantling?
- Which parts are wear items, and what are the lead times in your location?
- How are flexible connections arranged, and how long do they typically take to replace?
- Is the dust collector sized and instrumented for your product, and how is condensation avoided?
- What training and documentation come with the machine?
If your feed is sticky or prone to caking, see our guide to powder caking after drying, and for the machines themselves browse the GTI homepage.
Frequently asked questions
How often should a vibratory fluid bed dryer be serviced?
Follow the manufacturer’s manual. A common practice is daily walk-rounds and trend checks, weekly seal and damper inspection, and a detailed inspection at planned stops, adjusted with your own failure history.
What is the first sign of a blocked distributor plate?
A change in bed differential pressure at the same airflow and load, uneven moisture across the bed, or visible dead zones. Compare readings with your commissioning baseline.
How do I know if vibration is drifting?
Compare amplitude or motor current with your baseline for the same product and load, and look for new noise or loose mounts. Use the measurement method in your manual.
Why does the dust collector matter for dryer performance?
A loaded or damaged filter raises exhaust resistance and can reduce airflow through the bed. Wet or torn bags also release dust or blind the filter.
Can maintenance reduce energy use?
It can. Leaks, blocked plates, fouled heaters and failed steam traps all increase energy per kg of water removed. Tracking specific energy consumption shows when they develop.
Plan upkeep and spares with GTI
For assistance with dryer selection, maintenance planning, processing requirements or a project-specific quotation for a vibratory fluid bed dryer, contact Genex Tech Industries LLP (GTI Group).
Email: mktg@gtidryers.com
Call or WhatsApp: +91-93300 77417
Website: https://gtidryers.com/
Please share your material, required wet-feed capacity, initial and target moisture, available heating source and installation location.