When production volumes rise or product quality specifications tighten, many processors discover that batch tray drying becomes a bottleneck. Labour intensity, long cycle times, moisture variation between trays and limited scalability push plants toward continuous systems. A band dryer (also called a belt dryer, apron dryer or mesh belt dryer) is one of the most versatile continuous convective technologies for materials that can be spread in a uniform bed and conveyed through controlled drying zones.
This page is written for process engineers and technical buyers who need to decide whether a band dryer is the right solution, how to configure it correctly, and what problems to anticipate.
The Real Production Problem a Band Dryer Solves
Batch tray dryers work for small or highly variable lots. They become inefficient when:
- Throughput must increase beyond a few hundred kilograms per batch
- Final moisture must stay within a tight band across the entire product stream
- Colour, aroma or functional properties are sensitive to prolonged high-temperature exposure
- Labour cost and loading/unloading time dominate operating cost
- Integration with upstream cutting/washing and downstream cooling/packing is required
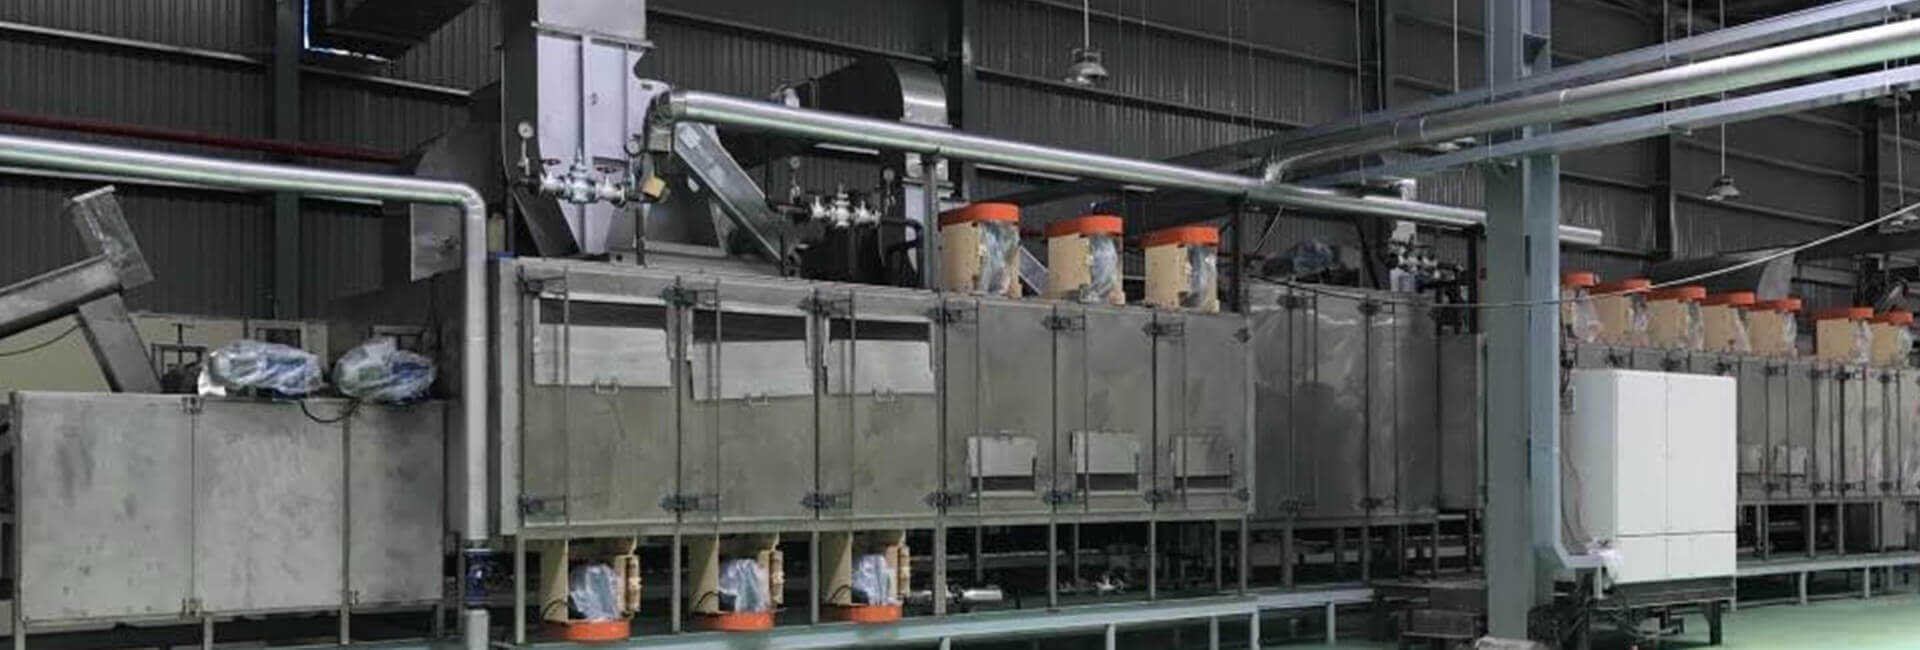
A continuous band dryer transports material on a moving perforated belt or metal apron through one or more insulated zones where heated air is forced through the product bed. Residence time is controlled by belt speed; temperature, airflow direction and humidity can be set independently in each zone. This staged approach is particularly useful for heat-sensitive or oil-rich materials that benefit from gentler initial drying followed by higher-temperature finishing.
According to established industrial drying literature, the conveyor dryer is conceptually simple yet one of the most versatile technologies available. It can handle a wide range of shapes, sizes and compositions while offering excellent control over residence time and drying conditions — provided bed loading, airflow distribution and zone design are engineered correctly.
How a Band Dryer Works – Process Fundamentals
- Controlled feeding and spreading
Wet material is distributed evenly across the full width of the belt at a controlled bed depth. Uniform loading is critical; uneven depth creates preferential airflow paths and moisture variation. - Multi-zone drying chamber
The product travels through single or multiple zones. Each zone can have independent temperature, up-flow or down-flow air, humidity and recirculation ratio. This allows the drying profile to match the changing moisture content of the product. - Convective heat and mass transfer
Heated air (steam coils, thermic fluid, hot-air generator or electric) passes through the product layer. Moisture is evaporated and carried away by the exhaust system. - Cooling and continuous discharge
An optional cooling zone reduces product temperature before discharge for packing, milling or further processing.
Typical process sequence:
Wet Feed → Even Spreading → Pre-Drying Zone → Main Drying Zone(s) → Final Drying / Conditioning → Cooling → Continuous Discharge
When a Band Dryer Is the Appropriate Choice
| Product / Process Characteristic | Band / Belt Dryer Suitability | Notes |
|---|---|---|
| Sliced, diced, shredded or particulate solids | Strong | Fruits, vegetables, spices, herbs, coconut chips/flakes/threads |
| Heat-sensitive or aroma-sensitive materials | Strong | Multi-zone control limits peak product temperature |
| Oil-rich products (e.g., high-fat desiccated coconut) | Strong with correct belt & airflow design | Gentle conveying reduces oil migration and sticking |
| Continuous high-throughput requirement | Strong | Designed for 24×7 operation |
| Need for precise residence-time control | Strong | Belt speed is a direct control variable |
| Free-flowing granules that fluidise easily | Moderate – evaluate fluid bed as alternative | |
| Very sticky pastes or filter cakes that cannot form a permeable bed | Weak – consider spin-flash, paddle or other technology | |
| Coarse bulk minerals or high-abrasion solids | Usually not first choice – rotary often preferred |
Common Process Problems and Engineering Responses
| Observed Problem | Typical Causes | Practical Engineering Response |
|---|---|---|
| Uneven final moisture | Non-uniform bed depth, blocked air ducts, uneven airflow distribution | Improve feeder/spreader design; verify zone balancing; measure airflow across belt width |
| Case hardening (dry surface, wet core) | Excessively high first-zone temperature or insufficient early-zone humidity control | Lower initial zone temperature; increase recirculation or humidity in early stages; extend residence time |
| Colour or aroma degradation | Prolonged exposure to high product temperature | Multi-zone profile with lower peak temperature; verify product temperature (not only inlet air temperature) |
| Belt tracking / deviation | Uneven tension, uneven loading, worn rollers, thermal expansion differences | Equalise tension; ensure level rollers; improve feed distribution; consider automatic tracking systems |
| Product sticking or belt blinding | Sticky intermediate moisture phase or oil migration | Correct belt material (mesh type, aperture); bed brushes or cleaning devices; optimise temperature profile |
| Low throughput or long drying time | Insufficient drying area, excessive bed depth, under-sized airflow | Recalculate evaporation duty; reduce bed depth or increase belt length/width; verify heat source capacity |
| High energy consumption | Excess exhaust, poor insulation, no heat recovery | Optimise recirculation ratio; add heat recovery; improve chamber sealing |
Laboratory or pilot trials with the actual feed material remain the most reliable method to confirm bed permeability, drying rate and final product quality.
Key Design Variables That Determine Performance
- Bed depth – Affects airflow resistance and drying uniformity. Too deep reduces permeability; too shallow reduces capacity.
- Belt type and aperture – Mesh, perforated plate or hinged apron selected according to particle size, stickiness and hygiene requirements.
- Number of zones and airflow direction – Single-pass multi-stage is the most versatile configuration for complex drying profiles.
- Belt speed – Primary control of residence time.
- Heat source and temperature profile – Steam, thermic fluid, hot-air generator or electric; product temperature must be distinguished from inlet air temperature.
- Exhaust and recirculation – Critical for energy efficiency and humidity control.
- Construction materials – Food-grade SS304/SS316 contact surfaces where required; CIP-ready options for hygienic applications.
Band Dryer vs Other Continuous Technologies
| Requirement | Band / Belt Dryer | Rotary Dryer | Fluid-Bed Dryer |
|---|---|---|---|
| Gentle handling of fragile or oil-rich pieces | Excellent | Moderate | Depends on particle strength |
| Multi-zone temperature & humidity control | Excellent | Limited | Good within fluidisation constraints |
| Continuous high capacity | Excellent | Excellent | Excellent for fluidisable solids |
| Precise residence-time control | Excellent (belt speed) | Moderate | Good |
| Materials that form a permeable bed | Strong | Not required | Requires fluidisable particles |
| Coarse bulk solids / minerals | Usually secondary | Strong | Possible |
| Sticky filter cakes | Limited | Limited | Limited – other technologies preferred |
There is no universal “best” dryer. Selection follows the physical state of the feed and the product quality targets.
Information Required for a Technical Assessment
To evaluate a band dryer correctly, the following data are needed:
- Product form (slices, dices, shreds, chips, granules, etc.) and particle-size range
- Incoming moisture (wet basis) and target residual moisture
- Required throughput (wet or dry solids basis)
- Maximum allowable product temperature or heat-sensitivity constraints
- Preferred heating medium and available utilities
- Hygiene or material-of-construction requirements
- Available footprint and integration with upstream/downstream equipment
- Any known problems with existing drying (uneven moisture, colour loss, sticking, etc.)
Illustrative mass-balance thinking (example only):
If 1 000 kg/h of wet product at 70 % moisture must reach 8 % residual moisture, approximately 675 kg/h of water must be evaporated. Actual dryer area, airflow and energy demand depend on drying rate, bed depth, temperature profile and heat losses — all material-specific.
How GTI Dryers Approaches Band Dryer Engineering
GTI Dryers designs and manufactures continuous band, belt, apron and mesh-belt drying systems for food, spice, coconut, pharmaceutical, chemical and biomass applications. Systems are engineered around the product’s bed-forming behaviour, moisture profile and quality requirements rather than a single standard machine.
Configurations can include multi-zone temperature and airflow control, adjustable belt speed, hygienic construction options and integration with feeding, cooling and exhaust systems. Capacity is customised according to process data; typical ranges referenced on GTI equipment pages start from pilot scale upward.
Pilot testing with representative feed is recommended before final equipment commitment.
Contact the GTI Technical Team:
Website: gtidryers.com
Band Dryer Page: gtidryers.com/band-dryer
Email: mktg@gtidryers.com
Phone / WhatsApp: +91 9330077417