In plastic recycling lines, washing removes labels, glue, dirt and other contaminants from PET bottles, HDPE containers, PP rigid scrap and mixed polymer streams. The washed flakes, however, leave the final rinse stage carrying a large amount of surface water — often 20–40 % moisture by weight.
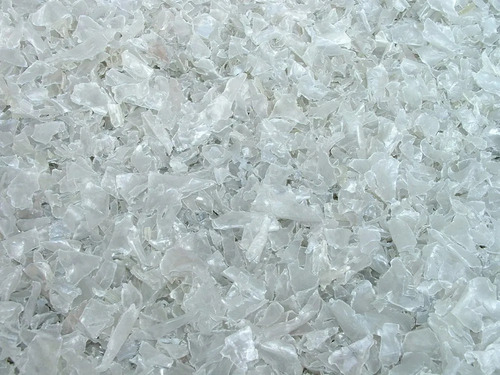
If this water is not removed efficiently before extrusion or pelletizing, the consequences are immediate: high energy consumption in the thermal dryer, residual moisture that causes hydrolytic degradation (especially in PET), foaming, strand breaks, reduced intrinsic viscosity and inconsistent pellet quality.
This page focuses on the engineering of the drying stage that follows washing in recycling plants. It builds on GTI’s broader polymer, resin and plastic drying content by concentrating specifically on post-wash flake drying for recycling lines.
The Core Problem: Surface Water After Washing
Washed plastic flakes are not the same as virgin pellets. The dominant moisture is free surface water held on and between the flakes. Thermal energy should not be the first tool used to remove this water.
An energy-efficient recycling line therefore follows a clear hierarchy:
- Mechanical dewatering (centrifugal dryer / spin dryer) – removes the bulk of free water at low energy cost
- Thermal surface drying (hot-air, fluid-bed or rotary) – reduces residual surface moisture to the level required by the next process
- Polymer-specific finishing (crystallization + desiccant drying for PET when needed)
Skipping or under-sizing the mechanical stage forces the thermal dryer to evaporate water that could have been removed mechanically, raising both capital and operating cost.
Typical Process Position in a Recycling Line
Baled scrap → Size reduction → Washing / friction washing / sink-float → Rinsing → Mechanical dewatering (centrifugal) → Thermal flake drying → (Crystallization for PET if required) → Storage / extrusion / pelletizing
The thermal dryer sits immediately after mechanical dewatering and must accept a continuous stream of damp flakes while delivering free-flowing material at the target residual moisture.
Dryer Technologies for Post-Wash Plastic Flakes
1. Fluid-Bed Dryer
Hot air passes upward through a bed of flakes, fluidising them and providing rapid surface-moisture removal. Vibration may be added for better transport.
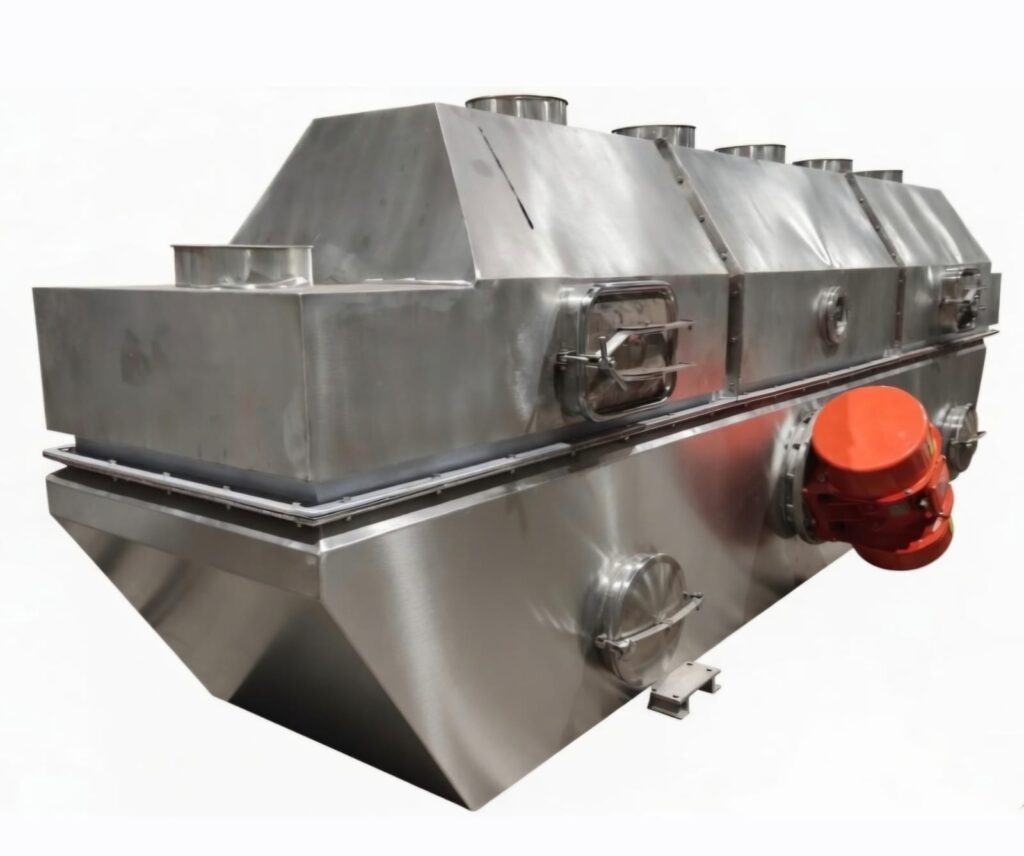
Strengths for recycling flakes
- Excellent gas–solid contact and moisture uniformity
- Continuous operation well matched to washing-line output
- Relatively gentle handling
- Can incorporate a cooling zone
2. Hot-Air / Pipeline Thermal Dryer
Flakes are conveyed pneumatically in a stream of heated air. Residual surface water evaporates during transport.
Strengths
- Simple integration after centrifugal dewatering
- Continuous and compact
- Effective for many rigid PET, HDPE and PP flakes
3. Rotary Dryer
A rotating drum with internal flights cascades the flakes through hot gas.
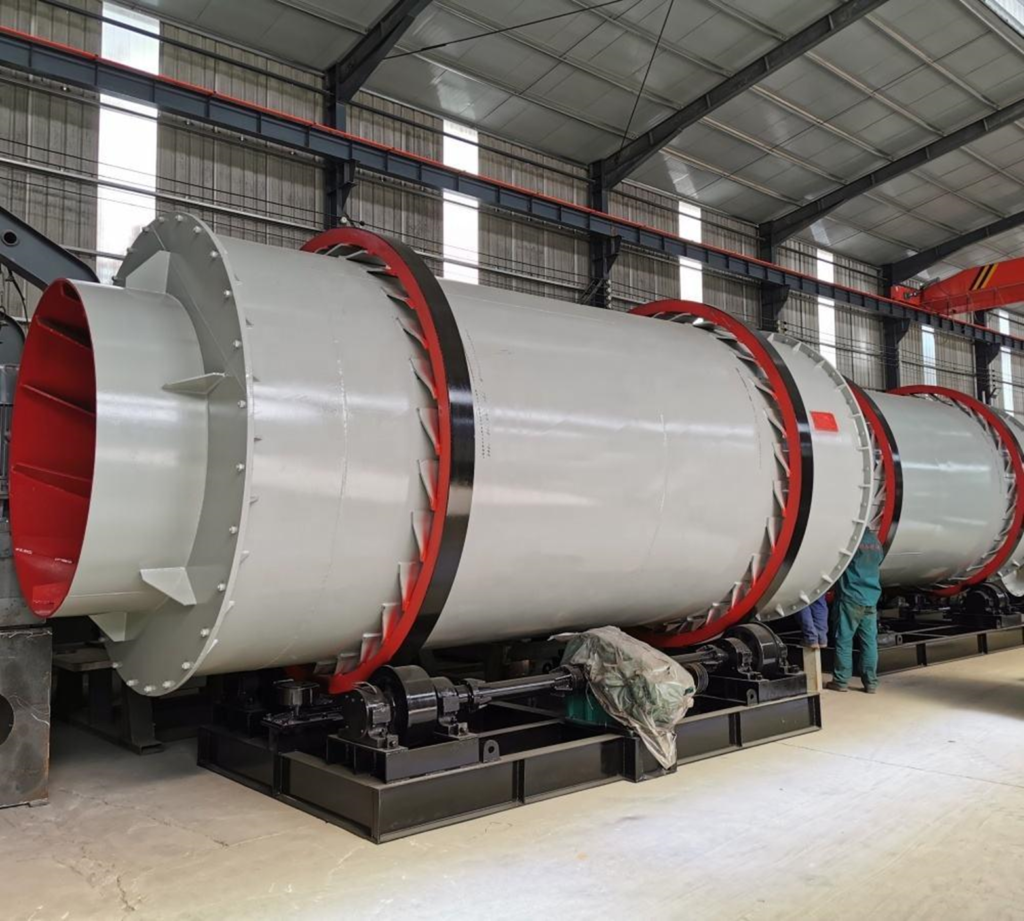
Strengths
- High continuous capacity
- Robust for mixed or irregular flake streams
- Proven industrial design
Design notes: Flight design and gas velocity must be chosen to minimise fines generation and avoid overheating thinner flakes.
Technology selection starting point
| Polymer / requirement | Preferred thermal approach after mechanical dewatering |
|---|---|
| PET flakes (general) | Hot-air / fluid-bed → optional crystallization |
| PET (food-contact / high IV) | Mechanical + thermal + crystallization + desiccant |
| HDPE / PP rigid flakes | Centrifugal + hot-air or fluid-bed |
| Mixed rigid flakes | Robust rotary or fluid-bed with good dust control |
| High-capacity lines | Continuous fluid-bed or rotary matched to washer output |
Critical Engineering Considerations
| Factor | Why it matters | Design implication |
|---|---|---|
| Inlet moisture after centrifugal stage | Determines thermal load | Target 1–3 % or lower before thermal dryer if possible |
| Target residual moisture | Depends on end use (extrusion, pelletizing, sale) | Define clearly; PET often needs much lower values than PE/PP |
| Polymer type | PET is hygroscopic and hydrolysis-sensitive; PE/PP mainly surface moisture | Different temperature and residence-time regimes |
| Flake size & thickness | Affects drying rate and risk of overheating | Adjust air temperature and residence time |
| Dust & fines | Thin flakes generate fines | Effective cyclone + filter system |
| Energy hierarchy | Mechanical water removal is far cheaper than thermal evaporation | Never omit or under-size centrifugal dewatering |
Common Problems and Engineering Responses
| Problem | Typical causes | Practical response |
|---|---|---|
| Residual moisture still high after thermal dryer | Mechanical dewatering inadequate; thermal dryer undersized | Improve centrifugal stage first; then re-evaluate thermal duty |
| PET IV drop / brittle pellets | Moisture too high at extruder | Tighten residual-moisture target; add crystallization + desiccant stage if required |
| Flake clumping or sticking (PET) | Amorphous PET heated above glass-transition without crystallization | Introduce crystallization step before high-temperature drying |
| High energy cost | Thermal dryer evaporating free water that should have been removed mechanically | Maximise centrifugal dewatering efficiency |
| Excessive fines | High gas velocity or aggressive cascading | Optimise air velocity and flight design; improve dust recovery |
| Uneven moisture | Poor feed distribution or short-circuiting | Improve feeder and bed/air distribution |
Key Data Required for Technical Assessment
- Polymer type(s) (PET, HDPE, PP, mixed)
- Flake size range after size reduction
- Moisture content immediately after washing and after centrifugal dewatering
- Target residual moisture for the next process
- Required throughput (kg/h or t/h)
- Downstream process (direct extrusion, pelletizing, sale of dry flake)
- Any food-contact or high-IV requirements (especially for PET)
- Available utilities and space constraints
Geographic Considerations & Market Evaluation
- India — Rapidly expanding plastic recycling capacity driven by EPR regulations and demand for recycled content; focus on robust, energy-efficient continuous systems matched to local washing-line outputs and power costs.
- Europe & North America — Emphasis on high-quality rPET (including food-contact), low residual moisture, energy efficiency and documented process control.
- Southeast Asia & other emerging recycling hubs — High-volume flake production; evaluation of cost-effective mechanical + thermal packages.
GTI evaluates each project from the actual post-wash moisture, polymer type and end-use specification rather than applying a single standard dryer.
How GTI Dryers Approaches Plastic Flake Drying in Recycling Lines
GTI Dryers designs industrial drying systems for polymers, resins and recycled plastics. For post-wash flake drying the engineering approach is:
- Treat mechanical dewatering and thermal drying as sequential, complementary stages
- Select fluid-bed, hot-air or rotary configurations according to polymer type, capacity and target residual moisture
- Pay special attention to PET (surface + absorbed moisture, crystallization needs)
- Integrate dust collection, product cooling and transfer to the next process step
- Support process-data review based on real washing-line outputs
This page strengthens GTI’s existing polymer drying content by providing a focused, recycling-line perspective on the critical post-washing drying step.
Frequently Asked Questions
Why is mechanical dewatering so important before thermal drying?
Free surface water can be removed mechanically at a fraction of the energy cost of thermal evaporation. A good centrifugal stage dramatically reduces the load on the thermal dryer.
What residual moisture is needed for PET flakes?
It depends on the end use. General extrusion may tolerate higher values; food-contact or high-IV applications often require very low residual moisture (tens to a few hundred ppm) and may need crystallization plus desiccant drying.
Can the same dryer handle PET, HDPE and PP?
A well-designed thermal dryer can process different rigid flakes, but operating temperatures, residence times and any crystallization step must be adjusted to the polymer.
Is a rotary dryer suitable for plastic flakes?
Yes for many high-capacity or mixed-flake applications, provided flight design and gas velocity are chosen to limit fines and overheating.
What information does GTI need for a quotation?
Polymer type, post-centrifugal moisture, target residual moisture, capacity and downstream process.
Contact the GTI Technical Team:
Website: gtidryers.com
Email: mktg@gtidryers.com
Phone / WhatsApp: +91 9330077417