
Fluid bed and vibratory fluid bed dryers (VFBD) rely on a stable, well-fluidised bed to deliver uniform heat and mass transfer. When fluidization fails — through channeling, dead zones, partial defluidization or uneven residence time — the result is moisture variation, local overheating, capacity loss and product quality problems.
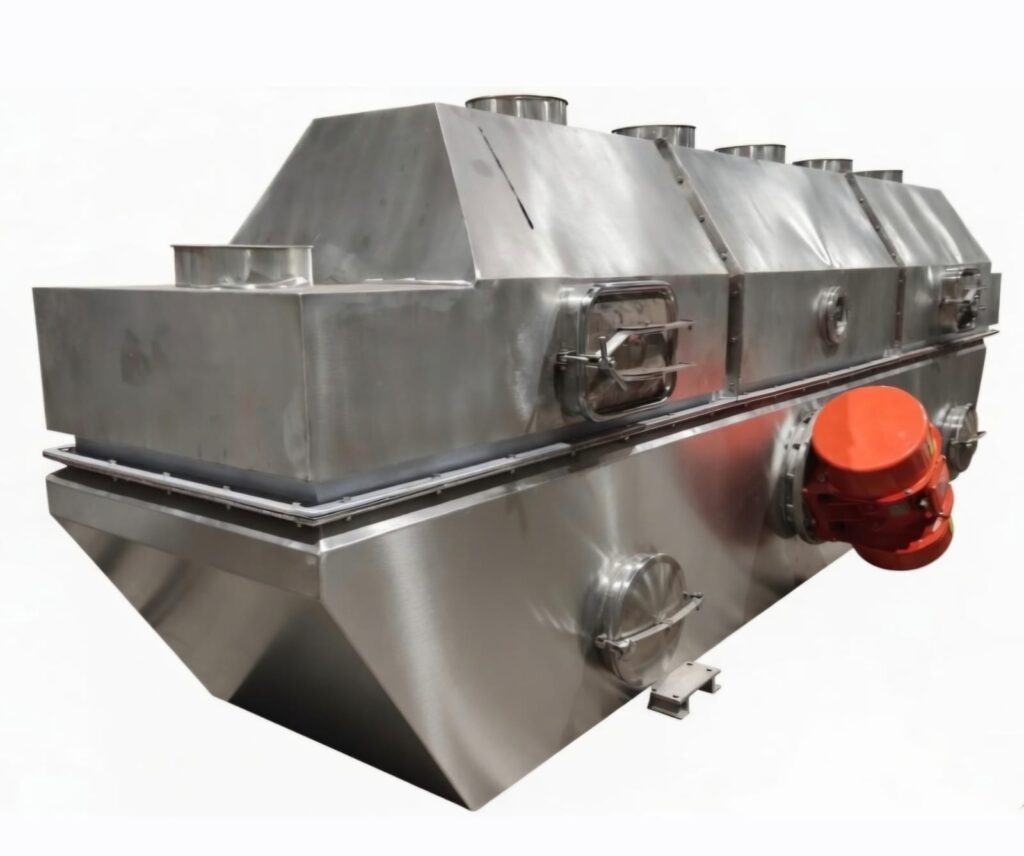
This guide is written for plant engineers and operators who need to diagnose the three most common performance complaints and decide whether the fix is operational, maintenance-related or a design limitation.
1. How a Fluid Bed Dryer Is Supposed to Behave
In a correctly operating fluid bed:
- Upward air velocity is high enough to suspend particles but not so high that large amounts of product are elutriated
- The bed expands and mixes continuously
- Gas and solids contact is relatively uniform across the distributor area
- Residence time is controlled by bed length, weirs, vibration (if VFBD) and feed rate
- Outlet moisture is consistent within the process tolerance
When any of these conditions break down, channeling, poor fluidization and moisture variation appear.
2. Problem 1 — Channeling
What operators see
- Preferential air paths through the bed
- Local “volcanoes” or jets of air
- Large areas of bed that look static or only weakly moving
- Higher pressure drop fluctuation or lower average pressure drop than expected
- Wet lumps or under-dried product in some fractions
Why channeling happens
| Cause | Mechanism |
|---|---|
| Incorrect air velocity | Velocity too low for the particle size/density → bed does not fully fluidise; air finds weak paths |
| Uneven distributor plate | Blocked, damaged or poorly designed perforations create preferential flow |
| Cohesive or sticky feed | Agglomerates form; air bypasses around them |
| Excessive bed depth | Pressure and resistance encourage channeling rather than uniform fluidization |
| Fines buildup or plate fouling | Open area reduced; local jets form |
| Poor feed distribution | Local overloading creates dense zones that resist fluidization |
Diagnostic checks
- Measure or estimate superficial air velocity and compare with the design or previous good operation.
- Inspect the distributor plate for blockage, warping or damaged holes.
- Check bed depth against design.
- Observe the bed surface: uniform bubbling/mixing vs fixed channels.
- Sample product from different locations (centre vs sides, inlet vs outlet) for moisture.
Corrective actions
- Restore design air velocity (fan speed, damper positions, filter condition).
- Clean or repair the distributor plate.
- Reduce bed depth if overloaded.
- Improve feed conditioning (break lumps, adjust moisture or additives if process allows).
- Ensure feed is spread evenly across the width.
- For cohesive products, evaluate vibration (VFBD), mechanical agitation aids or whether a fluid bed is the right technology.
3. Problem 2 — Poor Fluidization
What operators see
- Bed does not expand or “boil”
- Product remains as a static or only slightly mobile layer
- High pressure drop (bed packed) or very low pressure drop (air bypassing)
- Capacity well below design
- Frequent defluidization when feed rate or moisture increases
Why fluidization fails
| Cause | Mechanism |
|---|---|
| Air velocity below minimum fluidization velocity (Umf) | Particles not suspended |
| Particle size/density outside design range | Finer or denser product needs different velocity |
| High moisture or sticky surface | Particles bind; bed acts as a slab |
| Distributor design unsuitable | Insufficient pressure drop across the plate relative to the bed |
| Fan or filter limitation | Actual airflow lower than set point |
| Vibration settings incorrect (VFBD) | Vibration intended to help mobility is too low or wrong direction |
Diagnostic checks
- Confirm actual airflow (not only damper position or fan Hz).
- Compare current particle size and bulk density with the original design basis.
- Check inlet moisture and presence of lumps or binder.
- Verify distributor pressure drop and open area.
- On VFBD units, confirm vibration amplitude and frequency against commissioning settings.
Corrective actions
- Increase air velocity within the design envelope (watch elutriation).
- Reduce feed rate or bed inventory temporarily to re-establish fluidization.
- Improve upstream dewatering or lump breaking.
- Clean gas filters and check duct restrictions.
- Recalibrate or restore vibration parameters on VFBD systems.
- If the product has changed significantly (size, moisture, stickiness), request an engineering review — the original design may no longer match the feed.
4. Problem 3 — Moisture Variation
What operators see
- Wide spread in residual moisture between samples
- Some product over-dry (and possibly heat-damaged); some still above specification
- Downstream problems: caking, packaging issues, customer complaints
- Average moisture may look acceptable while variation is not
Why moisture varies
| Cause | Mechanism |
|---|---|
| Channeling or dead zones | Different particles see different gas contact time and temperature |
| Uneven feed rate or composition | Load and moisture swings along the dryer length |
| Poor temperature or airflow zoning | Final zones not finishing uniformly |
| Short-circuiting of product | Particles move too quickly along preferential paths (especially if weirs or vibration are wrong) |
| Segregation by size | Fines and coarse fractions dry at different rates |
| Sampling method | Samples taken from only one point hide the real spread |
Diagnostic checks
- Map moisture at multiple points (width and length) and on different size fractions if relevant.
- Confirm channeling or poor fluidization is not present (fix Sections 2 and 3).
- Check feed rate stability and inlet moisture variation.
- Verify zone temperatures and airflow balance.
- Review weir heights, bed level and vibration settings that control residence time.
Corrective actions
- Eliminate channeling and restore full fluidization first.
- Stabilise feed rate and inlet moisture.
- Adjust zone temperatures so the final zone finishes moisture without overheating already-dry material.
- Correct weir or vibration settings to avoid short-circuiting.
- Improve feed distribution across the dryer width.
- If size segregation is severe, consider whether screening or a different dryer type is needed.
5. Quick Diagnostic Flow
- Is the bed fully mobile and expanded?
- No → Focus on poor fluidization and channeling (air velocity, plate, feed condition, bed depth).
- Yes → Go to step 2.
- Is residual moisture consistent across locations and fractions?
- No → Check feed stability, zoning, residence-time control and sampling.
- Yes → Problem may be average moisture level (set points) rather than uniformity.
- Has the product or capacity changed since commissioning?
- Yes → Design basis may no longer apply; request engineering review.
- No → Focus on maintenance, air system and operating discipline.
6. When the Problem Is Design or Technology Fit
Operational fixes have limits. Consider design or technology review when:
- The product is cohesive or forms a paste-like bed that resists fluidization even at high velocity
- Particle size distribution is extremely wide and segregation cannot be controlled
- Required capacity forces bed depths or velocities outside stable fluidization
- Temperature sensitivity requires profiles that the current single-zone or poorly zoned unit cannot deliver
- Vibration (VFBD) is insufficient to keep the product mobile without damaging it
In these cases a different configuration (adjusted distributor, multi-zone design, VFBD vs static fluid bed, or an alternative dryer family such as belt or spin-flash) may be required.
7. Prevention — Operating and Design Discipline
- Commission and record the “good” operating window (airflow, bed depth, vibration, zone temperatures, feed rate).
- Trend pressure drop and exhaust temperature; sudden changes often precede visible channeling.
- Keep the distributor plate clean and inspect it on a planned interval.
- Control upstream moisture and lump content.
- Do not increase capacity only by raising bed depth or feed rate without confirming fluidization quality.
- Sample moisture from multiple points, not a single convenient location.
8. How GTI Dryers Approaches Fluid Bed Performance
GTI Dryers designs and manufactures fluid-bed and vibratory fluid-bed systems with emphasis on:
- Distributor design and air distribution for stable fluidization
- Multi-zone temperature and airflow control where product quality requires it
- Vibration parameters (for VFBD) matched to product mobility
- Clear operating windows based on process data
When plants report channeling, poor fluidization or moisture variation, GTI’s approach is to review feed characteristics, current operating data and machine configuration before recommending operational changes or design adjustments.
Geographic Note
Fluid-bed dryer problems appear in chemical, food, pharma, fertilizer and mineral plants worldwide. Ambient humidity, fuel type and seasonal feed variation can change the operating window, but the core mechanisms — minimum fluidization velocity, distributor quality and bed uniformity — are the same in every region.
Frequently Asked Questions
What is the first thing to check when channeling appears?
Actual air velocity and the condition of the distributor plate, followed by bed depth and feed condition.
Can vibration fix all fluidization problems in a VFBD?
No. Vibration helps mobility of cohesive or difficult products but cannot compensate for severe under-velocity, blocked plates or a fundamentally unsuitable particle size/moisture combination.
Why is average moisture on-spec but customers still complain?
Moisture variation across the product stream. Average can hide wet and over-dry fractions.
When should we stop adjusting and call for engineering help?
When the product or capacity has changed significantly from the original design basis, or when fluidization cannot be restored within the design air-velocity and bed-depth envelope.
What data should we send for a troubleshooting assessment?
Product type and particle size, inlet/outlet moisture targets, observed symptoms, current airflow/fan settings, bed depth, zone temperatures and any recent changes in feed or capacity.
Next Step
If your fluid bed or vibratory fluid bed dryer is showing channeling, poor fluidization or moisture variation, share the product data and observed symptoms. GTI can help diagnose whether the issue is operational, maintenance-related or a design/fit problem and recommend practical next steps.
Request a fluid bed dryer troubleshooting / performance assessment with your process data.
Contact the GTI Technical Team:
Website: gtidryers.com
Email: mktg@gtidryers.com
Phone / WhatsApp: +91 9330077417